A bolted flange joint looks simple: two flanges, a gasket and a ring of bolts. Yet leaking flanges remain a persistent cause of fugitive emissions, unplanned shutdowns and safety incidents. The difference between a joint that seals for years and one that weeps after the first thermal cycle usually lies not in the design, but in how it was assembled.
ASME PCC-1, Guidelines for Pressure Boundary Bolted Flange Joint Assembly, is the principal U.S. reference for assembling, disassembling and reassembling bolted joints in pressure equipment and piping. Unlike construction codes such as ASME B31.3 or Section VIII, PCC-1 is a post-construction guideline: it describes good practice that owner-users can adopt into their own procedures. It applies to joints using standard flanges such as those in ASME B16.5 and B16.47 as well as custom-designed flanges.
PCC-1 addresses the entire assembly process: training of personnel, cleaning and examination of flange faces, gasket installation, lubrication, tightening methods and patterns, target bolt load, and joint records. It also provides appendices on topics such as determining assembly bolt stress and alternative tightening patterns.
A gasketed joint seals because the bolts compress the gasket enough to fill the surface irregularities of the flange faces and to maintain that compression under pressure, temperature and external loads. Leaks generally arise from one or more of the following:
The single most important decision in assembly is the target bolt stress. Too little load and the gasket will not seal under operating conditions; too much and the gasket, flange or bolts may be damaged. PCC-1 provides guidance on selecting target assembly bolt stress, including a methodology that considers the maximum permissible gasket stress, the minimum gasket stress required to seal, and the allowable stresses in bolts and flanges. Many owner-users use this approach to set joint-specific values rather than relying on a single generic torque table.
When tightening by torque, the relationship between applied torque and bolt load depends on a nut factor that is highly sensitive to lubrication and thread condition. This is why PCC-1 emphasizes applying an appropriate, approved lubricant to the threads and nut-bearing surfaces, and using the nut factor associated with that lubricant.
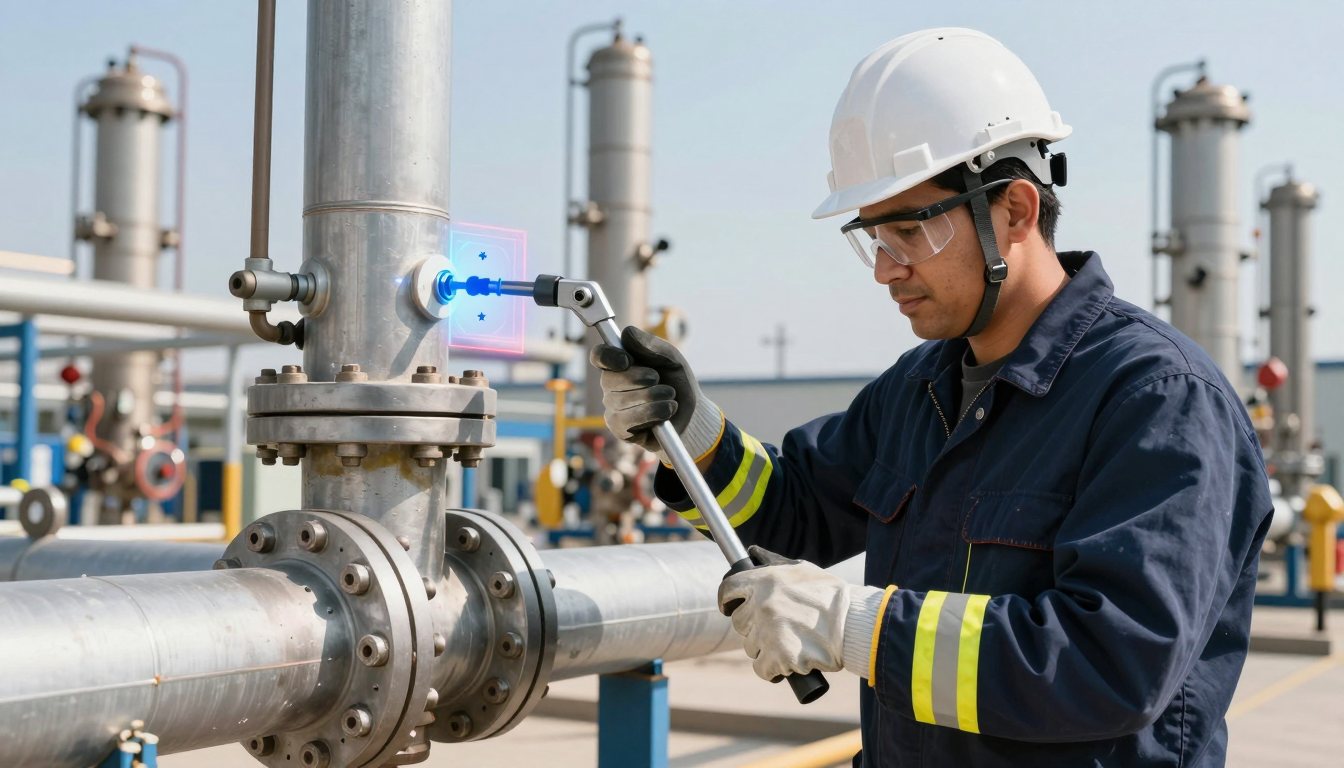
Bolt load can be applied by manual or hydraulic torque wrenches, by hydraulic bolt tensioners, or with load verified through ultrasonic measurement of bolt elongation. Each method has different accuracy and practicality, and PCC-1 discusses their relative merits.
The tightening sequence matters as much as the final value. PCC-1 describes a legacy cross-pattern (star pattern) approach in which the joint is first brought snug, then tightened in a series of incremental rounds of increasing torque following a cross pattern, followed by circular passes at the final value until no further nut rotation occurs. The guideline also presents alternative patterns that, when qualified for use, can reduce the number of passes while still achieving acceptable gasket compression. Whatever the method, the goal is uniform gasket compression around the circumference and parallel flange faces.
| Method | Principle | Typical considerations |
|---|---|---|
| Manual torque | Torque converted to tension through friction | Sensitive to lubrication; practical for small bolts |
| Hydraulic torque wrench | Controlled high torque output | Larger bolts; still dependent on nut factor |
| Hydraulic tensioning | Direct axial stretch, then nut run-down | Requires extra bolt length; load transfer losses must be accounted for |
| Ultrasonic elongation | Measures bolt stretch to infer load | Verification tool; requires calibration and access to bolt ends |
PCC-1 places strong emphasis on what happens before a wrench is applied. Flange faces must be cleaned and examined for damage within the gasket seating area; the guideline provides acceptance criteria for flange face imperfections and flatness. Fasteners should be checked for correct material, thread condition and freedom from damage. The gasket must be the specified type, new and undamaged, and centered properly. Flange alignment should be achieved without excessive force, because pulling misaligned piping together with bolts consumes load that should be seating the gasket.
A bolted joint is a system: flanges, fasteners, gasket, lubricant, procedure and people. Weakness in any one element will show up as a leak.
Recognizing that assembly quality depends on the assembler, PCC-1 includes an appendix on the training and qualification of bolted joint assembly personnel. It defines qualification levels — including the Qualified Bolting Specialist, Senior Qualified Bolting Specialist and Qualified Bolting Specialist Instructor — and describes the theoretical and practical content of training and the means of demonstrating competence. Many owner-users now require qualified personnel for critical joints such as those in high-temperature, hazardous or high-pressure service.
Best practice is to manage critical joints individually: identify them, specify assembly parameters for each, record who assembled them and how, and tag the joint after assembly. Such records make it possible to investigate leaks systematically and to refine procedures. Where a joint continues to leak, the response should include a review of design adequacy, not only retightening.
For hands-on competence in controlled bolting, consider IIME's Bolted Flange Joint Assembly per ASME PCC-1 training course.
 September 07, 2026 - BY Admin