High-density polyethylene (HDPE) pipe has become a mainstay of water, wastewater, gas distribution, mining and industrial systems because of its corrosion resistance, flexibility and fully restrained, leak-free joints. Those advantages depend on one thing above all: the quality of the fusion joint. A well-made butt fusion joint can match the strength of the pipe itself, while a poorly made one may pass a visual check and fail years later.
Butt fusion joins two pipe ends, or a pipe and a fitting, by heating the squared ends against a heater plate until a melt layer forms, removing the heater, and pressing the molten surfaces together under controlled pressure. The polymer chains of the two melt layers intermingle and, upon cooling under pressure, form a homogeneous joint. Unlike metal welding, no filler material is added; the joint is made entirely from the parent materials.
In the United States, the principal procedure standard is ASTM F2620, Standard Practice for Heat Fusion Joining of Polyethylene Pipe and Fittings. The Plastics Pipe Institute's PPI TR-33 provides a generic butt fusion procedure for polyethylene gas pipe, and internationally ISO 21307 describes several butt fusion procedures, including single low-pressure, dual low-pressure and single high-pressure methods.
The specified interfacial pressure is the pressure at the pipe-to-pipe interface, not the reading on the machine gauge. The gauge pressure is calculated from the interfacial pressure, the pipe end area and the effective piston area of the machine's hydraulic cylinders, plus the drag pressure required to move the carriage and pipe. Drag pressure must be measured for each joint, because a long string of pipe on the ground can require significantly more force to move than a short piece on rollers.
Fusion quality is the product of temperature, pressure and time, applied to clean, square, aligned surfaces. Lose control of any one and the joint is compromised.
The external bead tells a great deal about the joint. ASTM F2620 provides guidance on visual acceptance. A good joint shows a uniform double roll-back bead around the full circumference, with both halves similar in size and shape. The depth of the V-groove between the two beads should not extend below the pipe surface, and the joint should show no excessive high-low misalignment.
| Observation | Possible cause |
|---|---|
| Bead too small or V-groove too deep | Insufficient heat soak or fusion pressure; excessive open time |
| Bead excessively large | Excessive fusion pressure or heating time |
| Uneven bead around circumference | Non-square facing, misalignment or uneven heater temperature |
| Rough, sandpaper-like or pitted bead surface | Contamination, such as dirt or hydrocarbons |
| Unequal bead size between sides | Different materials or melt characteristics, or unequal heating |
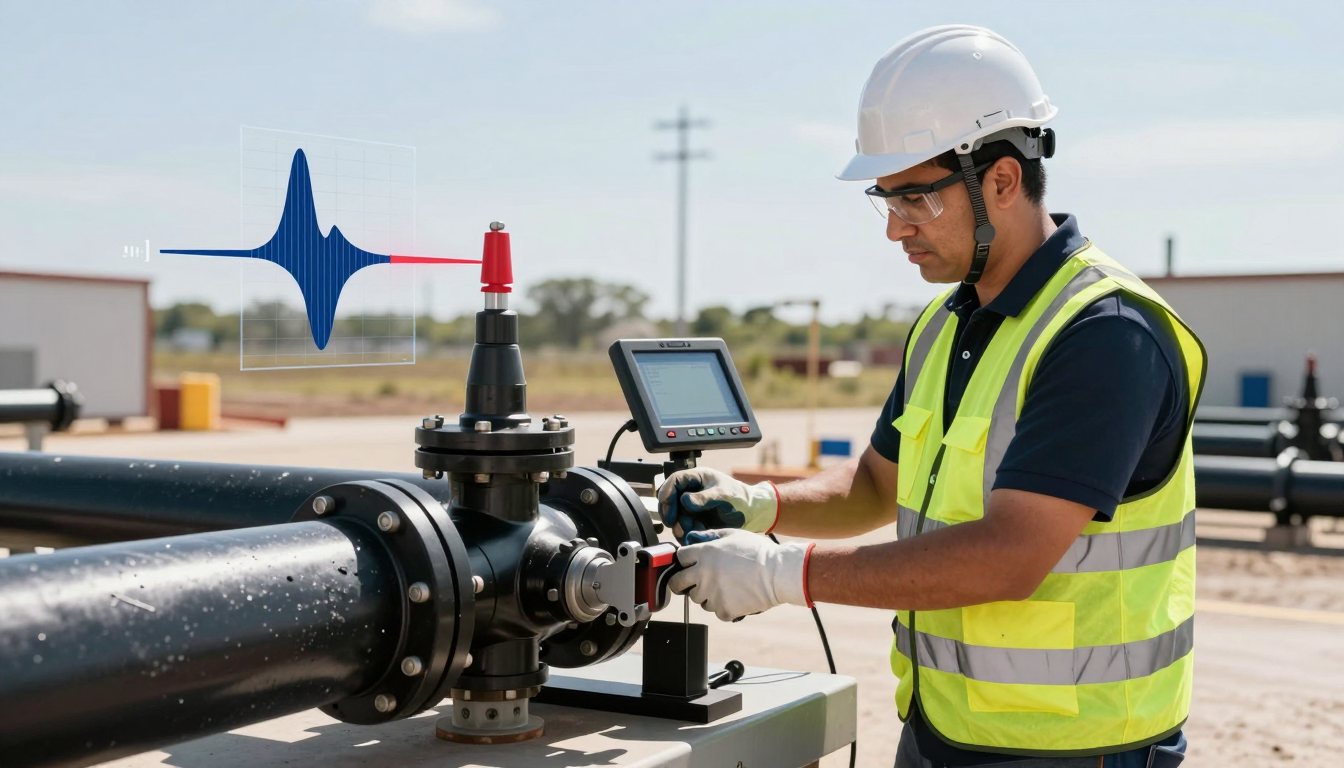
Electronic data loggers record heater temperature, pressures and times for each joint and compare them with the qualified procedure. Many owners require data logging on critical projects because it creates an objective record that visual inspection alone cannot provide.
Destructive tests are used to qualify procedures and operators and for periodic verification. Common tests include bend-back tests of straps cut from the joint, where the joint should not separate at the fusion interface, and the high-speed tensile impact test per ASTM F2634, which evaluates the ductility of the fusion interface. External beads may also be removed and bent to check for slits or voids.
Regulated gas pipelines in the United States must use joining procedures qualified under 49 CFR 192.283, and persons making joints must be qualified under 49 CFR 192.285. For pressure piping and power applications, ASME Section IX, Welding, Brazing, and Fusing Qualifications, includes rules for qualifying fusing procedures and fusing machine operators for polyethylene. Pipe and fitting manufacturers' recommendations, owner specifications and project requirements frequently add further controls.
Wind, rain, dust and extreme temperatures all affect fusion. Shelters protect the heater and the melt, and end caps reduce cooling drafts through the pipe bore. In cold weather, procedures may need adjustment to ensure adequate melt formation. Heater temperature must be verified regularly with a surface pyrometer, not only by the heater's own thermostat display.
To qualify your crews in polyethylene joining, explore IIME's HDPE Pipe Butt Fusion Operator training course.
 October 25, 2026 - BY Admin