Misalignment between coupled shafts is among the most common, and most preventable, causes of premature failure in rotating machinery. Flexible couplings tolerate some misalignment without complaint, which is precisely why it so often goes uncorrected. The bearings, seals and coupling components pay for it in reduced life.
Two coupled shafts are aligned when their rotational centerlines are collinear at operating conditions. Misalignment is described in two forms, each evaluated in both the vertical and horizontal planes:
In practice, most machines exhibit a combination of offset and angular misalignment in both planes. The alignment task is to measure all four values and correct them by moving the designated movable machine, usually the driver, with shims in the vertical plane and lateral moves in the horizontal plane.
A misaligned coupling transmits reaction forces and moments into the shafts as it accommodates the misalignment on every revolution. Those forces add to the loads carried by the bearings. The consequence is captured in the basic rating life equation for rolling-element bearings, defined in ISO 281:
L10 = (C / P)p, in millions of revolutions, where C is the basic dynamic load rating, P is the equivalent dynamic bearing load, and the exponent p is 3 for ball bearings and 10/3 for roller bearings.
Because life varies with load raised to the third power or more, modest increases in load produce disproportionate reductions in life. By the equation alone, a 10 percent increase in equivalent load on a ball bearing reduces calculated L10 life to about 75 percent of its original value, and a 20 percent increase reduces it to under 60 percent. Misalignment can also raise operating temperature, degrade lubricant and create uneven load distribution across rolling elements — effects that the basic rating equation does not capture and that further shorten service life.
Seals are equally vulnerable. Mechanical seals depend on precise face alignment, and shaft deflection driven by coupling forces can accelerate face wear and leakage.
Bearing life is governed by load raised to a power of three or more. That is why small alignment errors have large consequences, and why precision pays.
Vibration analysis often reveals misalignment through elevated vibration at one and two times running speed (1X and 2X), with significant axial components and phase differences across the coupling. Other indicators include high coupling temperatures, coupling wear debris, cracked or broken shafts near the inboard bearing, and repeated bearing or seal failures on the same machine. These symptoms overlap with other faults, so confirmation by measurement is essential.
| Method | Principle | Strengths | Limitations |
|---|---|---|---|
| Straightedge and feeler gauge | Visual coupling-rim and gap check | Quick, minimal equipment | Low accuracy; unsuitable for precision work |
| Rim-and-face dial indicator | Indicator readings on coupling rim and face | Well understood; no electronics | Bracket sag; face readings affected by axial float |
| Reverse dial indicator | Rim readings taken from each shaft onto the other | Good accuracy; less affected by axial float | Calculation or graphing required; bracket sag |
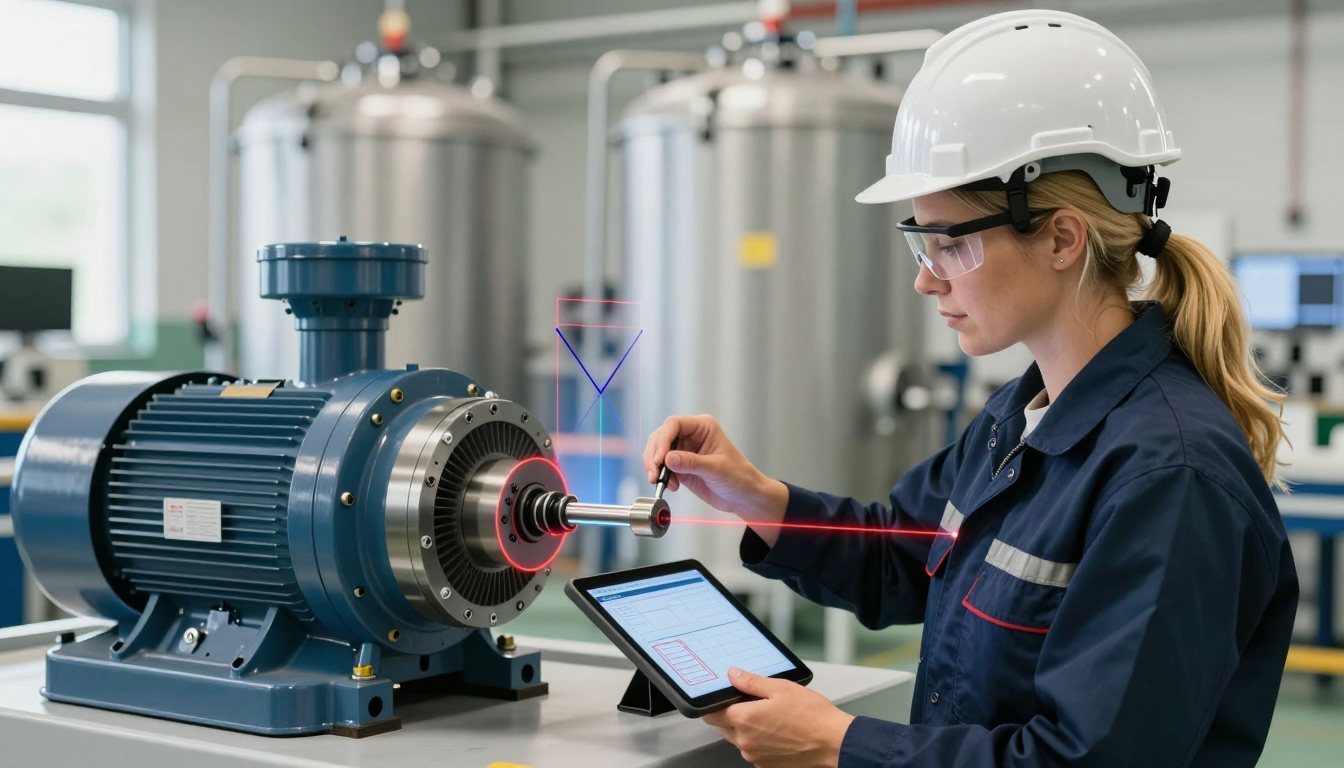
| Laser alignment | Laser and position detectors measure relative shaft positions during rotation | High resolution, no bar sag, real-time move guidance, documentation | Requires calibrated instrument and trained user; sensitive to air turbulence and heat shimmer |
Laser systems are now the common choice for precision work because they eliminate mechanical bracket sag, calculate corrections automatically, show live values during horizontal moves and produce records for trending. They do not, however, compensate for poor preparation.
Soft foot occurs when a machine foot does not sit flat on its base, so that tightening the hold-down bolt distorts the machine frame. It can distort bearing housings and change alignment readings as bolts are tightened. Checking each foot and correcting soft foot before final alignment is fundamental.
On pumps and compressors, piping forces can pull the casing out of position. Checking whether the shaft moves when piping flanges are loosened identifies pipe strain, which should be corrected in the piping, not by forcing the alignment.
Machines are aligned cold but run hot. Differential thermal expansion between a driver and a driven machine — for example, a hot pump and a cooler motor — changes shaft positions at operating temperature. Manufacturers often provide target cold offsets, and these can also be determined by measurement. The aim is alignment at operating conditions, not merely at rest.
Tolerances are typically expressed as allowable offset and angularity as a function of shaft speed, with tighter limits at higher speeds. ANSI/ASA S2.75-2017, Shaft Alignment Methodology, Part 1: General Principles, Methods, Practices, and Tolerances, provides a recognized basis, and equipment manufacturers' requirements should always be respected.
Use clean, precut stainless steel shims, minimize the number of shims under each foot, and ensure the base and machine feet are free of rust, paint and debris. Check for sufficient bolt-bound clearance before starting so that required horizontal moves are possible.
Recording as-found and as-left values, soft foot readings and thermal targets allows reliability engineers to correlate alignment quality with machine performance. Many organizations make precision alignment a standard step in any work that disturbs a coupling, and they verify it as part of commissioning.
To develop precision alignment skills, explore IIME's Laser Shaft Alignment and Precision Maintenance training course.
 October 13, 2026 - BY Admin